The core demand of steel structure manufacturers (especially PEB light‑steel and H‑beam workshops) is "cost reduction and efficiency improvement". The biggest pain points for factories are low welding speed (prone to undercut) and heavy labor consumption for post‑weld slag removal. In addition, steel plates in workshops often lack thorough grinding and carry mill scale or slight rust, which readily causes dense porosity.
We have developed a custom "ultra‑fast short‑slag" formula for steel‑structure workshops. It significantly refines the flux particle size (14‑60 mesh) to stabilize high‑current arcs for 1.6mm‑2.4mm fine wires, and enhances the intrinsic active deoxidizing capacity of the flux. Even on unground rust‑bearing steel plates, a travel speed of 0.8m/min‑1.3m/min can be achieved, and the slag curls up and spalls off automatically upon cooling.
Overseas customers fell into the "over‑specification" pit by using expensive high‑basicity extra‑low‑temperature fluxes (e.g. F7A5 class) for ordinary PEB building welding, which resulted in poor slag detachability. We delivered a well‑calibrated downgraded solution: high‑activity special steel‑structure flux matched with silicon‑free welding wire (to achieve optimal metallurgical balance). This greatly cut customers’ procurement costs and boosted workshop productivity by over 30%.
PEB Light‑Steel / Ultra‑Fast Twin‑Wire Fillet Welding:
GJ‑501A (PEB high‑speed custom version) + EM12 1.6mm‑2.4mm fine wire. The perfect synergy between silicon‑free wire and active flux enables grinding‑free operation and automatic slag removal.
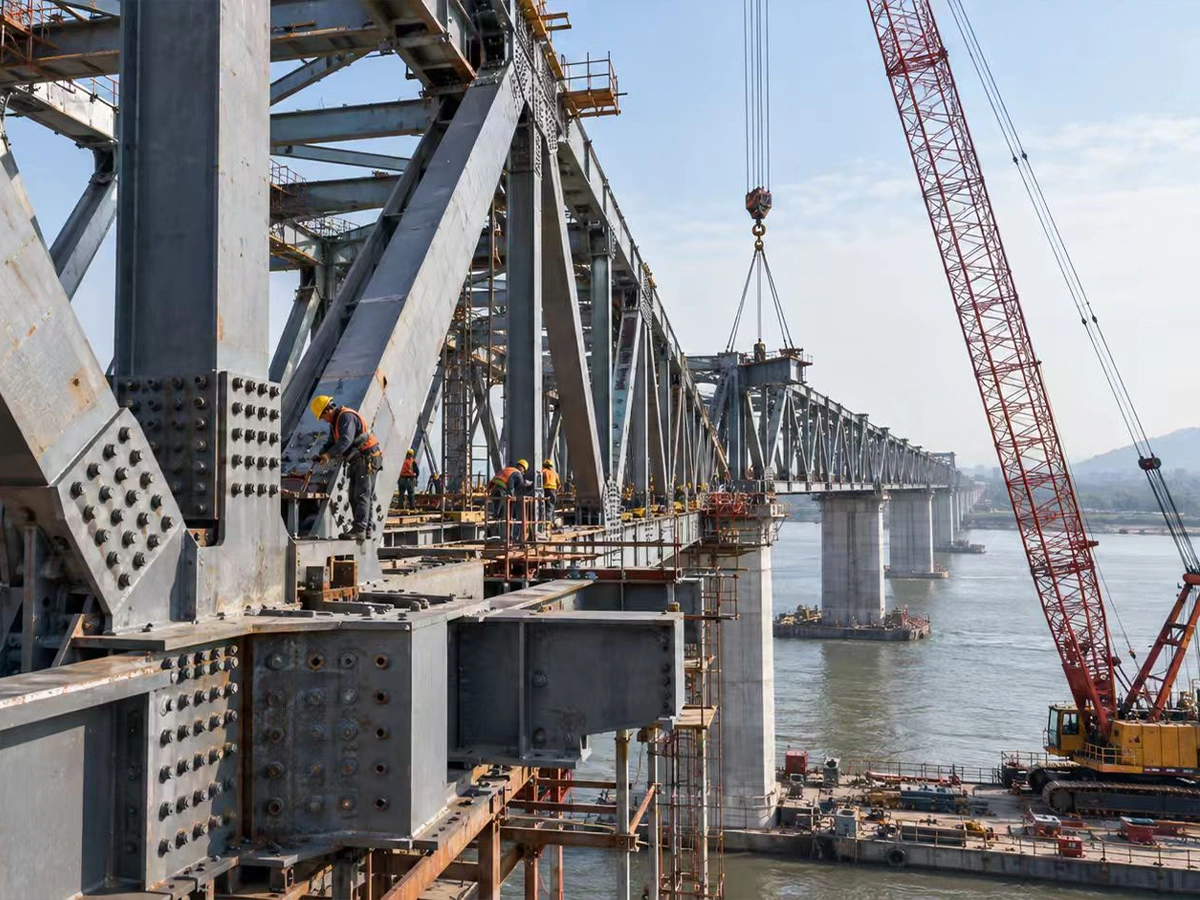
Heavy‑Duty Standard H‑Beams / Bridge Structures:
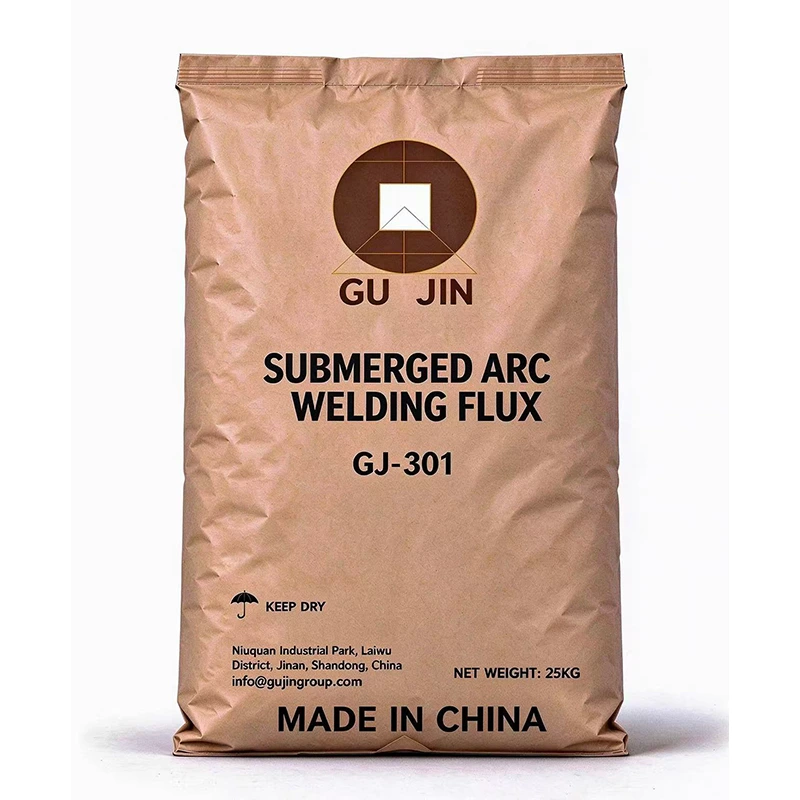
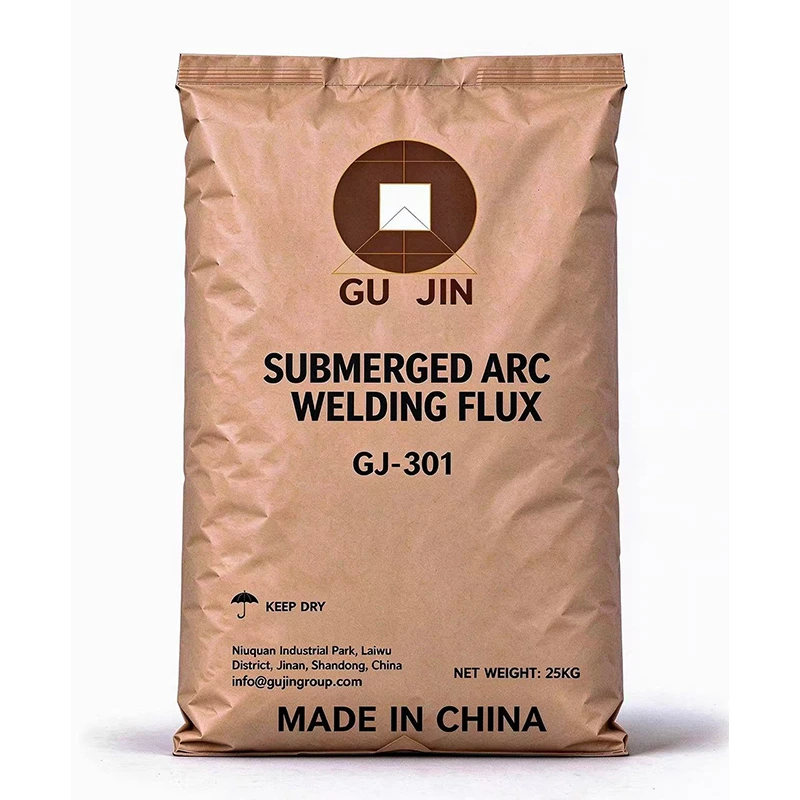
GJ‑301 (silicon‑calcium neutral type) paired with EM12K or EM13K welding wire. 1:1 equivalent to Lincoln 860 slag system, producing mirror‑smooth weld bead appearance
Copyright © 2026 by Jinan Gujin Welding Materials Co,. Ltd. All Rights Reserved