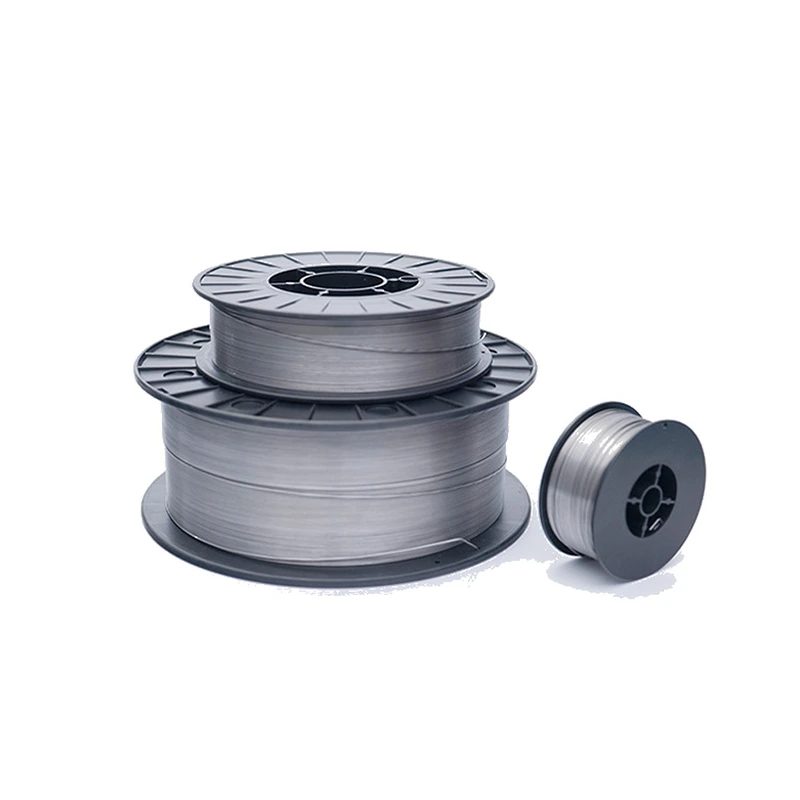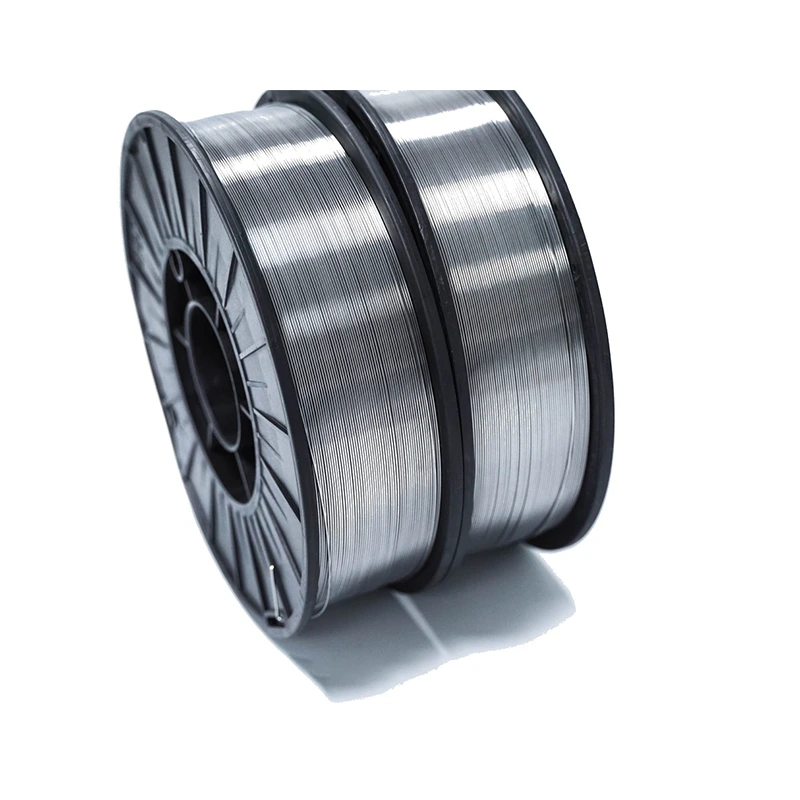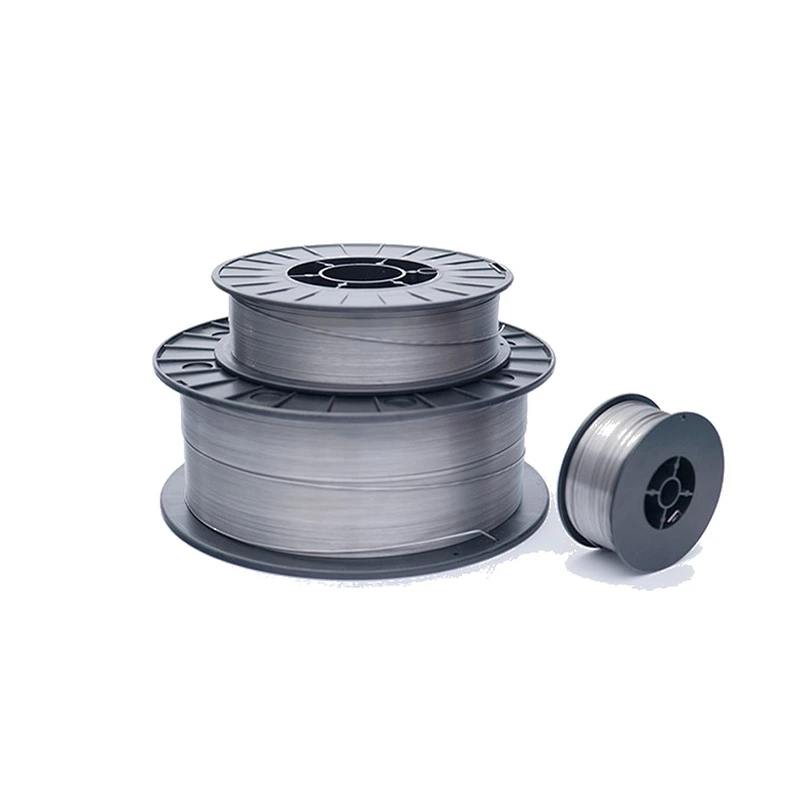
CO2 Gas-Shielded Flux-Cored Wire
(2.5Ni cryogenic low-alloy steel)
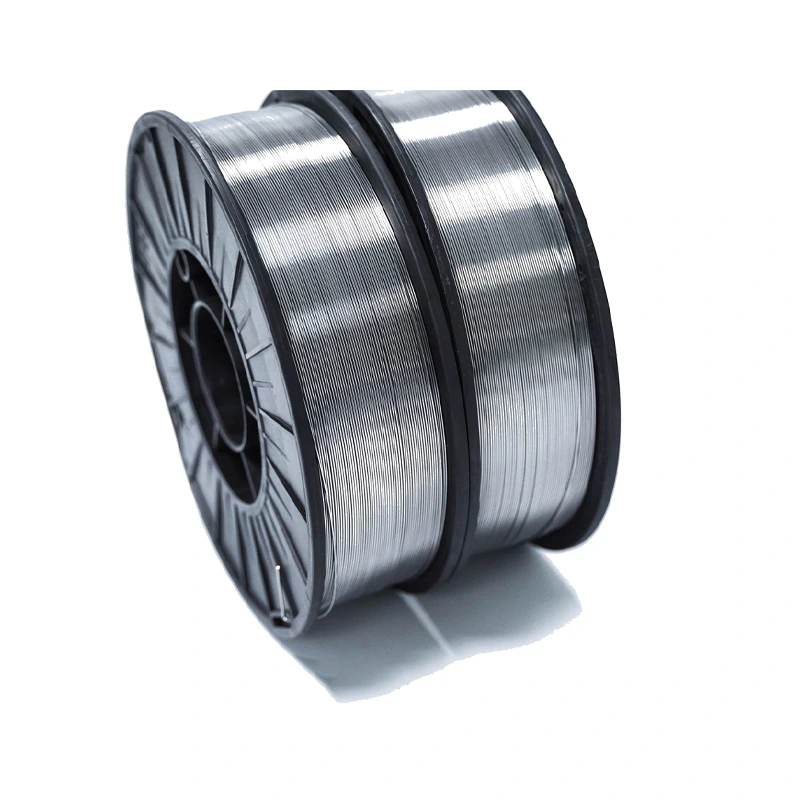
GJ-E81T1-K2C is a 2.5% nickel alloyed flux-cored wire strictly complying with AWS A5.29 E81T1-K2C. The high nickel content provides exceptional cryogenic toughness down to -60C, making it ideal for welding LNG storage tanks, cryogenic vessels, and arctic offshore structures.
Outstanding Cryogenic Toughness: 2.5% Ni composition delivers excellent Charpy impact values at temperatures as low as -60C.
High Strength & Ductility: Maintains 550MPa tensile strength with superior elongation for critical cryogenic service.
Low Hydrogen Design: Basic-rutile flux system ensures low diffusible hydrogen for maximum crack resistance.
With 100% CO2: For welding 2.5Ni and 3.5Ni steel cryogenic vessels, LNG storage tanks, and liquefied gas equipment.
For arctic offshore structures: Suitable for platforms and pipelines operating in extreme cold climate conditions.
For cold storage infrastructure: Ideal for refrigerated warehouses, cold boxes, and cryogenic process piping.
|
Elements |
C(Carbon) |
Mn(Manganese) |
Si(Silicon) |
Ni(Nickel) |
S(Sulfur) |
P(Phosphorus) |
|
AWS Requirement |
<=0.12 |
<=1.50 |
<=0.70 |
2.00 - 2.80 |
<=0.025 |
<=0.025 |
|
Typical Actual Value |
0.06 |
1.00 |
0.40 |
2.40 |
0.007 |
0.009 |
The mechanical properties of E81T1-K2C are tested as all-weld metal with 100% CO2 shielding gas (DC+ polarity).
|
Test Item |
Yield Strength |
Tensile Strength |
Elongation |
Impact Value@-60°C |
|
AWS A5.29 Requirement |
>=470 MPa |
550 - 690 MPa |
>=19% |
>=27 J |
|
Typical Actual Result |
520 MPa |
600 MPa |
23% |
85 J |
|
Wire Diameter |
1.0 mm (0.040") |
1.2 mm (0.045") |
1.4 mm (0.055") |
1.6 mm (1/16") |
|
Amperage |
80 - 180 |
140 - 300 |
180 - 340 |
200 - 400 |
|
Voltage |
18 - 24 |
22 - 32 |
24 - 34 |
26 - 36 |
Consistent Quality, Direct Factory Pricing.
 GUJIN
100% batch consistency ensured by our advanced in-house QA lab.
GUJIN
20+ years mastering SAW metallurgical synergy for heavy industries.
GUJIN
Full OEM empowerment, from custom formulations to private labeling.
GUJIN
Massive automated capacity to stabilize your bulk supply chain.
GUJIN
Long-term partner to hundreds of industrial conglomerates worldwide.
Moisture control is critical for submerged‑arc welding fluxes. Our standard packaging is 25‑kilogram multi‑layer kraft paper bags lined with heavy‑duty moisture‑proof plastic bags. For extreme environments or ultra‑low hydrogen requirements (such as H5 grade), we can also provide custom heavy‑duty aluminium foil vacuum packaging. All goods are stacked on wooden pallets and tightly wrapped with multiple layers of industrial shrink film to ensure 100% dryness upon arrival at the port.
No. For High-Grade Oil & Gas pipeline fabrication (such as API X60 to X70), standard neutral fluxes like 301 or active fluxes like 501 are not suitable, as they cannot guarantee the required extreme low-temperature impact toughness. You must use our dedicated pipeline-grade Fluoride-Basic agglomerated flux, GJ-101Q (or GJ-101G), combined with Mo/Ni-alloyed wires (e.g., EA2 or S3Ni1Mo).This combination ensures zero loss of alloying elements and guarantees impact values of ≥27J(or much higher) at -40°C to -50°C.
Our standard MOQ for international orders is normally 5 tons per item. For a full 20‑foot FCL container, the loading capacity is usually 24 tons subject to container space constraints, and it can reach 27 tons without pallets. A 40HQ high‑cube container can hold a maximum of 28 tons. Backed by our robust production capacity, we can finish production, quality inspection and packaging within 7‑10 days upon receiving the deposit, and deliver the goods to major Chinese ports such as Qingdao Port or Tianjin Port.
Yes! We fully understand that re-baking costs time and electricity. For customers who want to skip this step, we highly recommend selecting our Heavy-Duty Aluminum Foil Vacuum Packaging. The flux is vacuum-sealed immediately after high-temperature manufacturing. When you open the bag in your workshop, the flux is in a 100% factory-dry state and can be poured directly into the welding hopper for immediate use.
For structural steel with surface impurities like rust, oil, or mill scale, standard neutral or high-basic fluxes will likely cause porosity. You need our GJ-501A (Aluminate-Rutile Active Flux). It features a highly active deoxidizing slag system that offers exceptional tolerance to surface contaminants. This allows you to achieve flawless, X-ray quality welds at high speeds without rigorous pre-weld grinding, significantly boosting your shop floor efficiency.
Copyright © 2026 by Jinan Gujin Welding Materials Co,. Ltd. All Rights Reserved